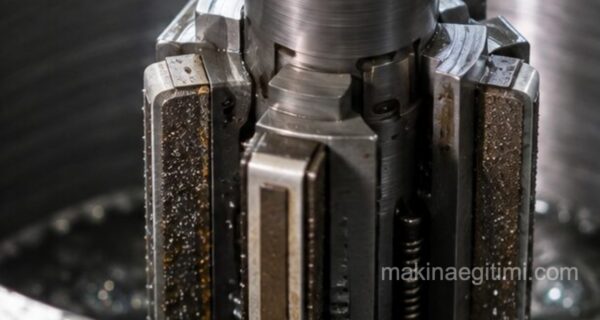
The operation of drilling a hole into the face of a workpiece with a special drill called a center drill, so that the part can be supported by the fixed and tailstock centers while rotating, is called drilling a center hole (making a center seat). Center holes are also called center seats. A center hole is a special countersink with a blind hole matching the shape of the center’s tip.
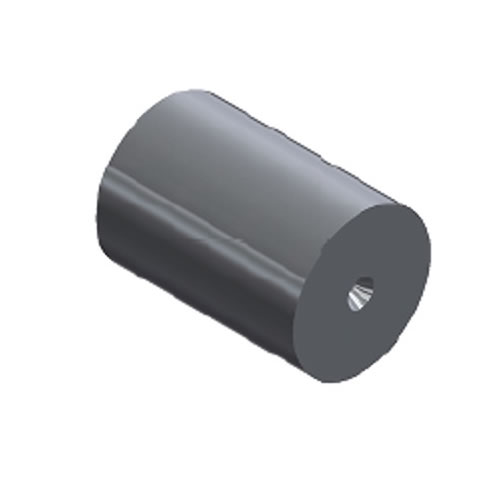
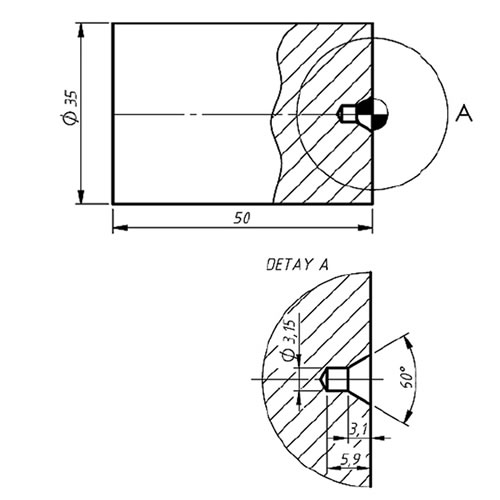
A center hole is drilled to support, seat, and center a workpiece that needs to be mounted long (between the chuck and the tailstock) by the tailstock. This way, the workpiece is centered and rotates without runout during turning.
A center hole can sometimes also be drilled as a pilot hole when drilling large-diameter holes. Specially manufactured center drills are used to drill these holes. Center holes can generally be drilled on lathes, drill presses, automatic (screw-machine) lathes, milling machines, and similar machines.
Types of Center Drills

Standard (plain) center drill: The tip of the drill cuts a 60° conical countersink. This drill is used for all kinds of parts.
Bell (protected-countersink) center drill: In addition to the 60° conical countersink, the tip of the drill also cuts a 120° protective countersink. This drill is preferred for heavy and large workpieces.
Radiused center drill: The drill tip is curved and cuts a convex countersink at a 60° taper. This drill is chosen for turning operations done using a traveling (following) center.
When selecting a center drill for workpieces that need a center hole, the workpiece’s diameter is taken into account, and a center drill appropriate for the workpiece’s diameter is selected from tables. Selecting the right center drill and drilling it correctly is important for turning operations to be carried out properly.
Job of the Center Hole
A center hole is a conical seat that allows long parts to be supported by the tailstock center during turning.
Center Drill Angle
Standard center drills are generally manufactured with a 60-degree taper angle.
Need for Low Speed
When drilling with a center drill, a low spindle speed should be preferred to prevent the drill from breaking.
Steps for Drilling with a Center Drill
- The workpiece should be mounted in the chuck as short as possible and running true.
- The face of the part should be faced off so that no nub remains.
- The chuck is fitted into the tailstock, and the center drill appropriate for the workpiece is mounted into the chuck.
- The tailstock is advanced so the center drill’s tip approaches the part, and the tailstock is locked in place.
- The spindle speed appropriate for the center drill’s diameter is calculated, and the approximate value is set on the machine.
- The machine is started. The tailstock handwheel is turned by hand to bring the drill toward the work.
- A few drops of oil are applied to the tip of the center drill, and the drill is fed at a steady speed to the desired depth.
- If the other end also needs a center hole, the part is turned around and the same operation is repeated.
Video of Drilling a Center Seat on a Lathe
Why Does a Center Drill Break
Causes of a center drill breaking:
- A nub remaining at the center of the face.
- The workpiece being mounted with runout.
- The drill running with runout due to incorrect adjustment of the tailstock and chuck.
- Incorrect spindle speed and feed rate.
- Not using cutting fluid.
Calculating Lathe Spindle Speed for Center Drilling
Example: A center hole needs to be drilled in a Ø45x200mm part so it can be supported by the tailstock. The part’s material is Ç1050 (C1050 steel), the cutting speed is 20 m/min, and the center drill diameter for an A-type center is Ø4mm. Calculate the spindle speed accordingly.
V= π . d . n / 1000
20= 3.14. 4 . n /1000
20000 = 3.14. 4. n
20000 / 12.56 = n
n = 1566 (rounded to the nearest, 1600 rpm)
Related Questions
If a long part is held only by the chuck while being turned, it can wobble. A center seat allows the tailstock center to support the part from its other end as well, letting the part rotate without runout and in a balanced way.
A standard drill only cuts the 60-degree countersink that the center’s tip will seat into. A bell-type drill additionally cuts another 120-degree countersink, preventing the edge of the center seat from getting damaged by impacts.
Related Posts