

When we compare deep-drawing dies to piercing, blanking, bending, and similar dies, we see some differences. Despite the experiments carried out to date and the experience gained as a result, producing non-symmetrical vessels with deep-drawing dies is not easy. For this reason, for a good deep-drawing die design to be made, the designer needs to
have sufficient knowledge and skill in deep-drawing die design, and needs to take the following process sequence into consideration.
1) — Design of the vessel to be drawn,
2) — Planning of the process stages,
3) — Design of the drawing dies,
4) — Selection of the press machine that will perform the drawing operation,
5) — Study of the manufacturing methods and working principles of previously made drawing dies.
After gathering information that can help solve any problems that might arise during production, work should proceed to manufacturing the drawing die.
Drawing Stages in Deep-Drawing Dies

Shows in how many stages a shaped vessel to be produced with cylindrical drawing dies can be drawn. In the first drawing operation, strip material or round sheet blank material suited to the dimensions of the vessel to be drawn is prepared. The prepared round sheet blank is placed inside the die.
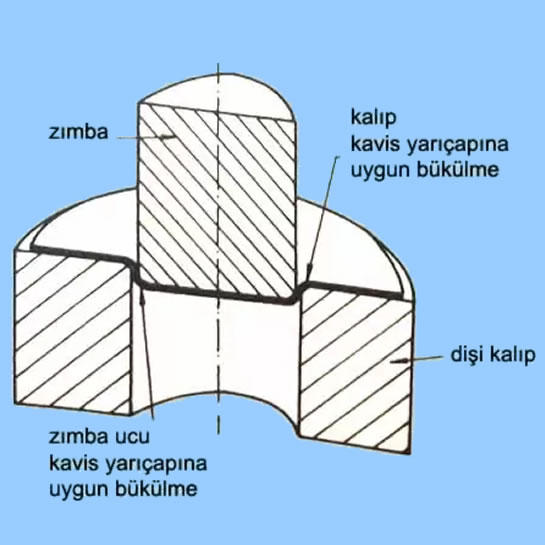
No change occurs in the sheet material until the punch, sheet material, and die come into contact. The moment the punch starts advancing into the die, the sheet material bends according to the radius of the punch tip.
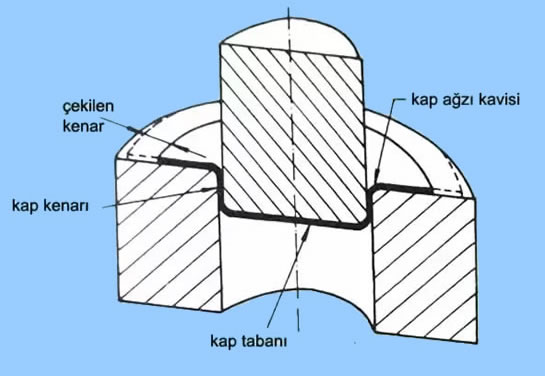
As the punch continues to advance, no shape change occurs in the base of the drawn vessel. However, the part that was bent according to the radius of the punch tip and die opening begins to straighten out. During the drawing operation, the diameter of the round sheet blank also decreases.

Compressive stress occurs on the outer periphery of the round sheet material flowing (advancing) into the die. This compressive stress causes material buildup in the flange section near the mouth of the drawn vessel. This kind of material buildup is called wrinkling.
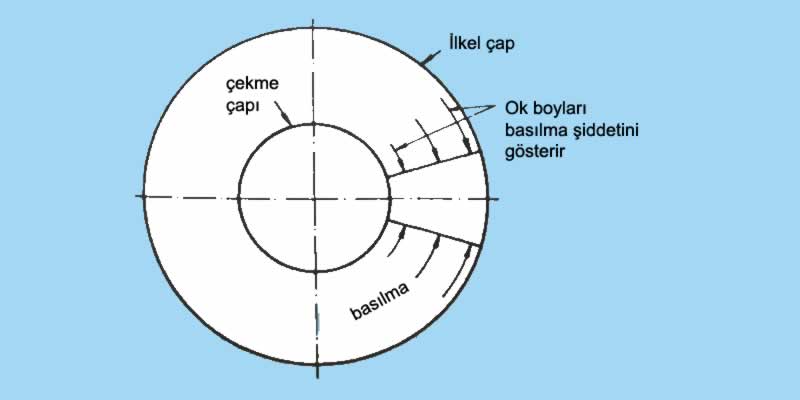
Wrinkling occurs at the mouth of the drawn vessel, along with a thickness increase of about (15%–20%)T. Additionally, bending and compressive stresses occur on the curved surfaces at the mouth and base of the finished vessel, while maximum tensile stress occurs in the areas near the base. In these areas where the tensile stress is at its maximum, the wall thickness of the drawn vessel decreases, and when the part is subjected to excessive drawing, tearing zones form around the base.

Related Posts
 Spinning Mandrels and Spinning Machines
 Centering Pin Dimensions and Assembly in Dies
 Drawing Defects in Drawing Dies and How to Resolve Them
 Die Clamping on Eccentric Presses
 Parts of Eccentric Presses
 Die Guide Pillars and Bushings
 Blank Holder Plates and Ejector Plates in Blanking Dies
 Compound Dies