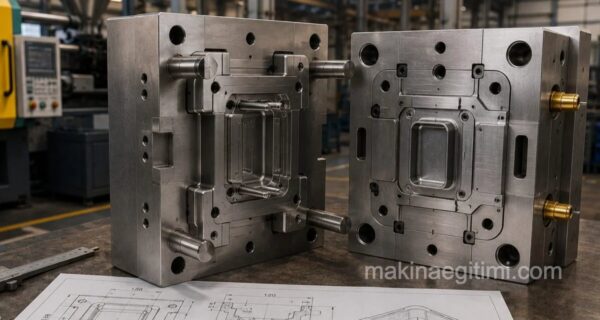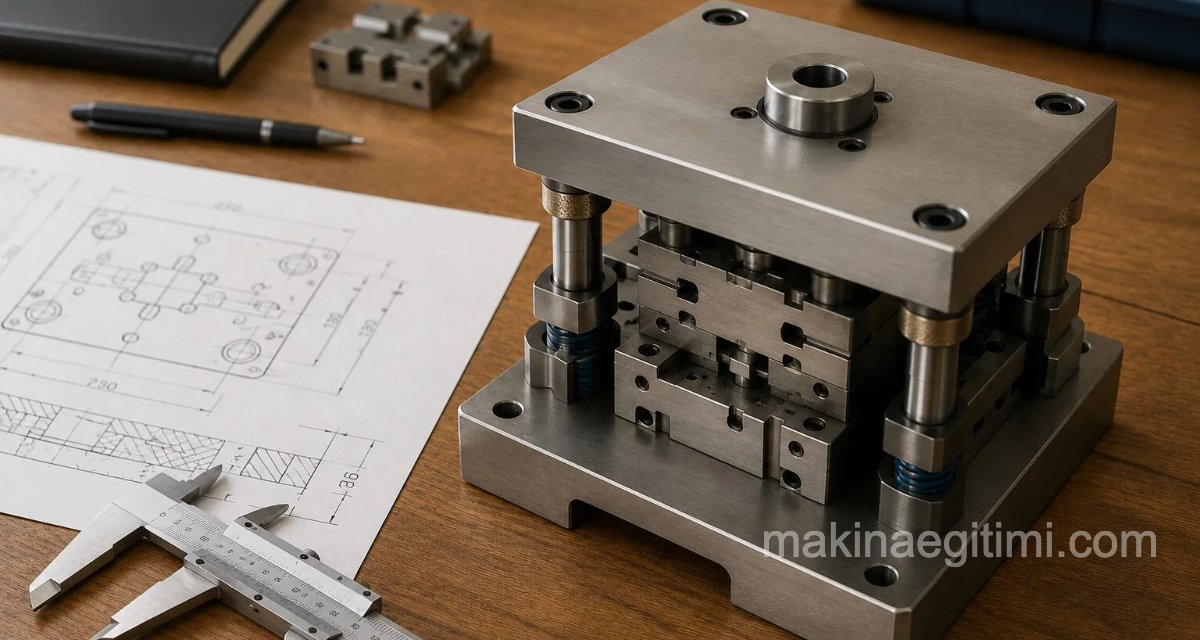
Die plates are made from carbon or alloy steels that can be hardened in water, oil, or air. These steels have a tensile strength above 40 kg/mm².
Depending on the shape of the part to be formed, die plates are made either as a single piece or as a segmented (multi-piece) assembly. We can explain the reasons for making segmented die plates as follows.
- Die plates that are much larger than a certain size are not made from a single piece,
- Die plates that are difficult to machine are made in multiple pieces,
- For die plates used in producing large quantities of small parts, this simplifies assembly and reduces cost,
- It’s easy to reuse pieces from one die to another in different forming operations.
- Where standardized die plates are commercially available for the application, segmented die plates are preferred.
Design of Segmented Die Plates
The following points should be kept in mind when designing segmented dies;
- Each piece should be large enough to be assembled independently with a sufficient number of bolts and pins.
- Each piece should be able to undergo heat treatment on its own.
- It should be kept in mind that breakage or wear will be greater at keyway or edge-cutting sections of the die.
- Segmented die pieces should be fitted to each other as precisely as possible.
- The mating surfaces of segmented die pieces should be at 90°.

Two-piece die plate design, preferred and non-preferred cases. (figure above)

A typical multi-piece die plate design (above)

Table 1: Table of the primary base dimensions for die plate sizing, based on sheet material thickness (above)
The sizes of small and medium-sized die plates are found using the previously tested and proven values in the table above. For larger die plates, a strength calculation is performed and the dimensions are determined accordingly.
Small and medium-sized die plates are divided into 3 main groups based on the shape of the part being formed.
- Die plates with a round forming hole,
- Die plates with a smooth-edged forming hole,
- Die plates with a sharp-edged forming hole.
The position of the part to be formed on the die plate is determined in advance by drawing a layout. To fully draw out the part’s layout plan on the die plate, the strip material cutting allowance is found based on the sheet material thickness and part dimensions, by referring to the tables below.

Table of cutting allowance amounts based on strip material thickness. DIN 3367 (Above)

Table of cutting allowance (b) amounts in single and double side-gauge dies, based on strip material thickness (Above)
Based on the forming steps, the primary base dimensions for the die opening (l and l1) are calculated.
The distance from the die opening to the edge of the die plate (A) is selected from the table above. According to the known values, the part’s production layout is transferred (traced) onto the die plate.
Calculating Die Plate Dimensions
Based on the values found from the layout plan above, and taking into account the distances from the die opening to the edge of the die, the die plate dimensions (X and Y) are calculated.
The die plate thickness is likewise selected from the table above, based on the thickness of the sheet material.
The dimensions of die plates to be used in high-tonnage forming operations are found using beam-strength formulas.

Based on the die plate’s mounting position and the acting forming force (P), the die plate’s dimensions are found by applying the formulas given in the table above.

Calculation and formulas for the section modulus and moment of inertia of some beams (above)
Punch dimensions are also calculated using the section modulus and moment of inertia formulas above.

The primary dimensions for die plate sizing are given above.
Example Problems for Calculating Die Plate Dimensions
Question 1

The part with the given dimensions will be produced with a compound piercing-and-blanking die. Prepare the die plate layout plan and find its dimensions. (The part will be produced from St 42 sheet material with a thickness of T = 2 mm.)
Solution:
Based on the dimensions of the part to be formed, the primary base dimensions for the die opening (l and l1) are found. Then the distances from the die opening to the edge of the die are found using Table 4, or with the help of coefficient K from the diagram below.

Die plate dimension X = A + A₁ + L mm
Die plate dimension Y = A + A + L₁, mm
A₁ = 40 x 0.67
A₁ = 26.8 mm is found
Die plate length, from the formula X = A + A₁ + L mm,
X = 27+26.8+41.5
X = 95.3 mm
Die plate width, from the formula Y = A + A + L₁, mm,
Y = 27+27+40
Y = 94 mm is found.
To find the die plate thickness, the forming force is found first. Forming force = the total piercing and cutting perimeter length of the formed part x sheet material thickness x the sheet material’s shear strength.
Accordingly;
Forming force P = Lt . T . Td, kg
T = 2mm Td = 42 kg/mm² Lt = 170mm,
P = 170 . 42 . 2
P = 14280 kg
From Table 5:
Mb (max) = P . L / 4
Mb (max) = 14280 . 40 / 4
Mb (max) = 142800 kg·mm
From Table 5, setting the product of the die plate section modulus, W = b . h² / 6, and the die plate’s bending stress equal to the die plate’s bending moment gives the following result.
Mb (max) = σb . W. From this, 142800 = σb . b . h² / 6. For the die plate, σb = 30 kg/mm², b = 27 mm, and substituting the die plate thickness (B) for h in the formula gives;
Die plate thickness

B = 32 mm is found.
SOLUTION 1
Since the strip material thickness is T = 2 mm, using Table 2, the cutting allowance b = 2.5 mm is found.
The primary base dimension for the die opening lengthwise: l = 41.5 mm
The primary base dimension for the die opening crosswise: l1 = 40 mm
From Table 5:
A=38 mm and A1= 32 mm
die plate length X = 38+32+41.5
X= 111.5 mm
die plate width Y = 2 X 38+40
Y=116 mm
From Table 1, die plate thickness B=28 mm
SOLUTION 2
Based on the primary base dimensions for the die opening, coefficient K is found from the diagram above. The primary base dimension for the die opening is then multiplied by coefficient K, giving the distance from the die opening to the edge of the die (A).
Since l = 41.5 mm, K = 0.65
Since l1 = 40 mm, K1 = 0.67
A = l x K
A1 = l1 x K1
A = 41.5 x 0.65
A = 27 mm is found.
Related Posts