

Stripping Force. The total friction force between the punch stripper (guide) plate and the punch is called the stripping force. The stripping force is taken as a percentage of the strip material thickness and the total forming force, using the constant (K) from the table below. Or, as a practical rule, the constant (K) is taken as between 1/40 and 1/5 of the total forming force.
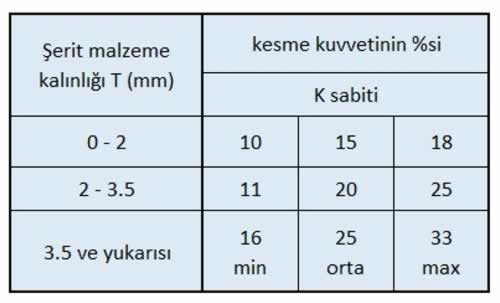
We can find the stripping force using the formula below.
Ps = K . P (kg)
P = Lt . Td . T (kg)
Ps = K . Lt . Td . T (kg)
Ps = Stripping force (kg)
K = Percentage of the total forming force (from the table above), or taken as between 1/40 = 2.5% and 1/5 = 20% of the total forming force.
Punch Buckling Length Calculation
Small-diameter or small-cross-section punches used in piercing and blanking dies need to pierce or cut without buckling. For this, the maximum punch length is calculated. The calculation is done according to the “EULER” equation. The critical loading formula Euler’s equation applies to beams can also be applied to punches in the same way.

The image above shows the beam loading configuration and Euler’s equation.
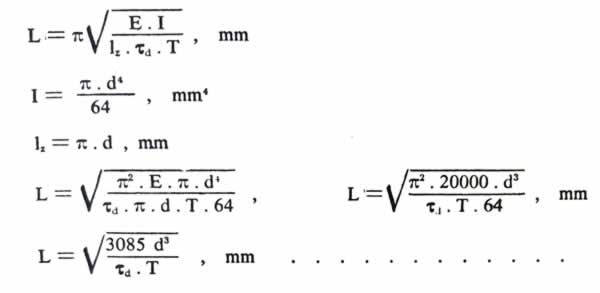
From the formula, the punch’s cutting force can be written as Pz = lz . Td . T, kg. One end of the punch is fixed (either pinned or rigidly fixed) to the punch plate, while the other end is supported by the guide plate. When we set the punch’s cutting force equal to “Euler’s” equation in figure a above, we can write the following formula.
Pz = Pkr is written.
Pz = lz . Td . T, kg

This gives us the equation.

E = Modulus of elasticity of the punch material, kg/mm2
L = Punch length, mm
I = Moment of inertia of the punch, mm4
lz = Cutting perimeter length of the piercing or blanking punch, mm
Pkr = Euler critical load, kg
π = 3.14
Since the punch material is made from hardenable steel materials, the modulus of elasticity can be taken as E = 20000 kg/mm2. The punch’s moment of inertia is calculated based on the punch’s cross-section.

Some punch cross-section profiles and their moments of inertia are given in the table above.
Accordingly, for a round-section punch with a modulus of elasticity of E = 20000 kg/mm2, the buckling length is found with the formula below.
Sample Application: Die Cutting Force, Stripping Force, and Buckling Length Calculation
The washer shown, with the given dimensions, is to be mass-produced from 3 mm thick aluminum material using a piercing-and-blanking progressive die. (Td= 10kg/mm2) Accordingly;

- Find the maximum cutting (forming) force.
- Given a safety factor of N = 1.5, find the safe forming force.
- Find the cutting work.
- Find the stripping force.
- Find the buckling length of the piercing punch.
SOLUTION
Maximum cutting (forming) force:
LT = π . (D+d)
LT= 3.14 (26+14) = 125.7 mm
P = LT . Td . T
P= 125.7 x 3 x 10 =3750 kg
Safe forming force:
Pem = P . N
Pem = 3750 x 1.5 = 5625 kg
WORK(die) = P( 1 — % P.D.R) T, kg.mm
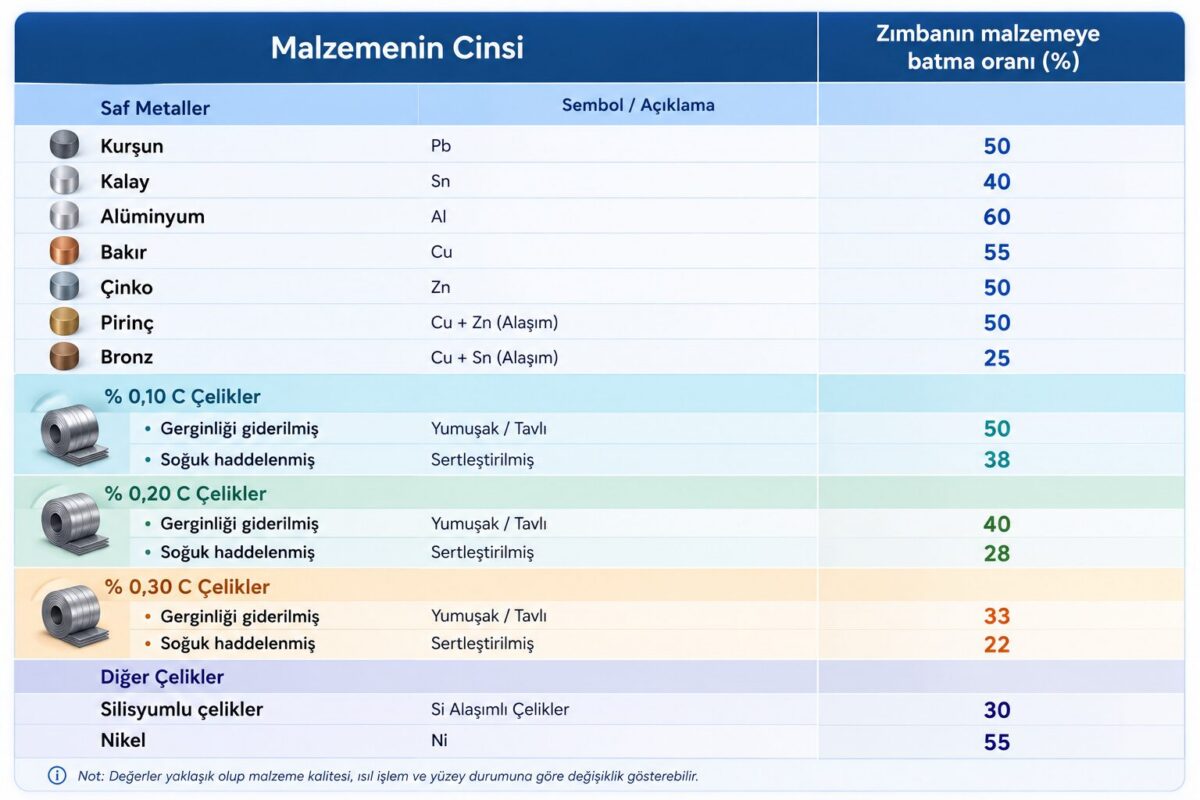
From the punch penetration ratio table above, % P.D.R = 60%
WORK(die) = 5625 (1—0.60) . 3 , kg.mm
WORK(die) = 6750 kg.mm
Stripping force:
Ps = Pem x K or Ps= (2.5%— 20%) x Pem
Ps= 5625 x 0.20 = 1125 kg
Buckling length: from the formula
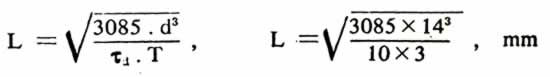
L= 531 mm is found.
Related Posts
 Calculating the Amount of Springback in Bending Dies
 Trimming (Correction) Amount in Drawing Dies
 Standard Die Sets and Their Dimensions
 Transfer Molding and Transfer Molding Dies
 Press Operator Training Notes
 Cooling System in Plastic Injection Molds
 Spinning Mandrels and Spinning Machines
 What Is Aluminum Extrusion, How Is It Done?