Close Menu
  • MAKİNELER ve İMALAT
    • Tools & Equipment
    • Computer-Aided Drawing
    • CAD/CAM Education
    • CNC Machine Programming
    • Casting Technologies
    • Electrical & Electronics Technologies
    • Hydraulics & Pneumatics
    • Manufacturing Processes
    • Manufacturing Technologies
    • Occupational Safety
    • Mold & Die Design
    • Solid Modeling
    • Welding Technology
    • Machine Elements
    • Mechanical Trade Drawing
    • Materials Science
    • Automotive & Vehicle Technologies
    • Robotics Technologies
    • Health Technologies
    • Defense & Aerospace Technologies
    • Descriptive Geometry
    • Technical Drawing
    • Software & Hardware Technologies
    • Innovative Manufacturing Methods
  • TEKNOLOJİ ve YAŞAM
    • OTOMOBİLLER ve TAŞIT
      • Vehicle & Engine Knowledge
      • Safe Driving
      • Sürüş Destek Sistemleri
    • Genel Kültür
      • Movies & TV Shows
      • Görsel ve Grafik Sanat
      • Books & Literature
      • Music
      • Sports
      • History
      • History of Technology
    • GÜNDELİK YAŞAM TEKNOLOJİLERİ
    • Hobbies & Entertainment
    • Internet Technologies
    • Health
    • Mobile Technologies
Makine Eğitimi
  • Machines & Manufacturing
    Machine Elements
    Hydraulics & Pneumatics
    Technical Drawing
    Computer-Aided Design & Manufacturing
    Basic Manufacturing Processes
    Manufacturing Processes
    Industry Technologies
    Other Technical Courses
    Motion & Power Transmission
    Simple Machines
    Chains & Sprockets
    Shafts & Journals
    Gears
    Cams
    Couplings
    Belts & Pulleys
    Springs
    Bearings
    Keys
    Fastening Joining
    Retaining Rings
    Screws, Bolts & Nuts
    Cotter Pins
    Flanges
    Welding
    Rivets
    Pins & Bolts
    Washers
    Calculators
    Gear Ratio Calculator
    Spring Constant Calculator
    Belt Pulley Ratio Calculator
    Other Machine Elements
    Slides & Linear Guides
    Brakes
    Flywheels
    Clamps
    Shock Absorbers
    Gaskets & O-Rings
    Seals & Sealing Elements
    Hydraulics
    Introduction to Hydraulics & Principles
    Hydraulic Systems & Applications
    Accumulators
    Filters
    Motors
    Pumps
    Valves
    Pneumatics
    Introduction to Pneumatics & Principles
    Pneumatic Systems & Applications
    Pneumatic Circuit Components
    Valves
    Cylinders
    Silencers
    Motors
    Compressors
    Dryers
    Conditioning Units
    Common Topics & Maintenance
    Hydraulic & Pneumatic Maintenance
    Study Notes, Exams & Tests
    Technical Drawing
    Introduction to Technical Drawing
    Geometric Drawings
    Perspective & Projection
    Orthographic Views
    Dimensioning
    Sectioning
    Assembly & Detail Drawings
    Tolerances
    Surface Finish Symbols
    Mechanical Engineering Drawing
    Screws, Bolts & Nuts
    Pulley Drawings
    Gear Drawings
    Shafts & Journals
    Bearing Drawings
    Pins & Bolts
    Spring Drawings
    Welds in Technical Drawing
    Washers
    Cotter Pins
    Technical Drawing Exercises
    Mechanical Drawing Exercises
    Gear Exercises
    View Extraction Exercises
    Pulley Exercises
    Pin & Bolt Exercises
    Threaded Fastening Exercises
    Descriptive Geometry
    Computer-Aided Drawing
    AutoCAD Drawing Lessons
    Computer-Aided Drawing Exams
    Solid Modeling & Animation
    Solid Model Drawing Files
    Solid Model Assembly Examples
    Solid Model Drawing Lessons
    3D CAD Software Reviews
    Solid Modeling Exercises
    CNC Programming
    CAM
    Measurement & Inspection
    Dial Indicators
    Calipers
    Gauges
    Micrometers
    Materials Science
    Steels
    Cast Iron
    Aluminum
    Plastics
    Material Testing & Hardness Measurement
    Occupational Safety
    Workshop Safety
    Safety When Working With Electricity
    Machine Safety Rules
    Hand Operations
    Filing
    Marking
    Cutting Operations
    Reaming
    Tapping
    Threading With a Die
    Drill Bit Sharpening
    Working With Machines
    Basic Turning Operations
    Basic Milling Operations
    Shaper Machine
    Machining
    Turning
    Milling
    Grinding
    Innovative Manufacturing Methods
    EDM (Electrical Discharge Machining)
    Laser Machining
    Waterjet Machining
    3D Printing
    3D Scanners
    Welding
    Rolling
    Casting
    Mold & Die Design
    Mechanical & Hydraulic Presses
    Blanking & Piercing Dies
    Bending Dies
    Drawing Dies
    Plastic Injection Molds
    Extrusion Dies
    Compound Dies
    Progressive Dies
    Blow Molds
    Spinning Dies
    Spray Molds
    Manufacturing of Machine Parts
    Automotive & Vehicle Technologies
    Motor Vehicle Manufacturing
    Raw Material Production
    History of Technology
    Health & Medical Technologies
    Defense & Aerospace
    Robotics Technologies
    Software & Hardware Technologies
    Mechanics - Strength of Materials
    Physics Topics
  • Technology & Life
    Hobbies & Entertainment
    Sports
    Music
    Vehicle & Engine Knowledge
    Vehicle Maintenance & Repair
    Safe Driving
    Driver Assistance Systems
    History
    Movies & TV Shows
    Books & Literature
    Computers & Internet
    Computer Tips
    Software Reviews
    Hardware & Peripherals
    Practical & Safe Internet Use
    Visual & Graphic Art
    Mobile Technologies
    Travel
    Science
    Health
    First Aid Knowledge
    Everyday Technologies
Makine Eğitimi
Home»Manufacturing Technologies»Progressive Dies
30 August 2026Updated:15 September 2026

Progressive Dies

Ardışık Kalıplar hakkında bilgi

Dies that produce parts requiring more than one forming operation, worked in sequence at separate stations, are called progressive dies (progressive mold / progressive die stamping).

  • Design of Progressive Dies
    • Related Videos
  • Related Questions

In progressive dies, each processing stage of the part being produced is completed at a separate station. In some cases, empty (idle) stations can be included within the die. This prevents the female die from being weakened and makes assembling the punches easier. However, this increases the length of the die set.

Progressive dies are generally used when mass production volume is very high and the cost of the part to be produced is low. Otherwise, designing and building a progressive die for stamping parts with low production quantities will increase the cost of the die as well as the cost of the stamped part.

Progressive stamping and strips

The figure above shows the stamping positions on the strip material for a part produced in a simple pierce, blank, and part-off progressive die.

Design of Progressive Dies

The person designing a progressive die must demonstrate their knowledge and skill, and should also draw on previously built progressive die designs along with their own experience.

The following process steps should be kept in mind when designing progressive dies.

1- The sheet material thickness should not be too small.
2- Die set dimensions suited to the available press machine should be chosen.
3- The total forming force must not exceed the tonnage of the available press machine.
4- Pilot holes and notches used for guiding purposes should be placed at the first station, and other piercing, blanking, bending, drawing, and similar operations should be done at subsequent stations.

5 — The strip material used for drawing or forming operations should be prepared to the appropriate dimensions.

6 — If a part requires a large number of piercing operations, these operations should be distributed across several stations.

7 — In simple pierce-and-part-off progressive dies, to increase the female die area, piercing should be designed at the first station, an idle second station, and the part-off operation at the third station (Figure 10.11-b).

8 — An idle station should be included to ease the movement of the strip material and increase the strength of the female die, stripper, and punch plates.

9 — The rolling direction of the strip material should be indicated.
10- Whether the drawing or forming operation will be in the downward or upward direction should be designed in advance.

11- Depending on the shape of the part being produced, any other operations preceding the cutting operation must be clearly specified.

12 — The strip-material feed mechanism should be selected to suit the die design.
13 — To minimize material waste, the strip layout plan should be prepared in several different configurations.
14 — The cutting or forming area suited to the press force must be specified.
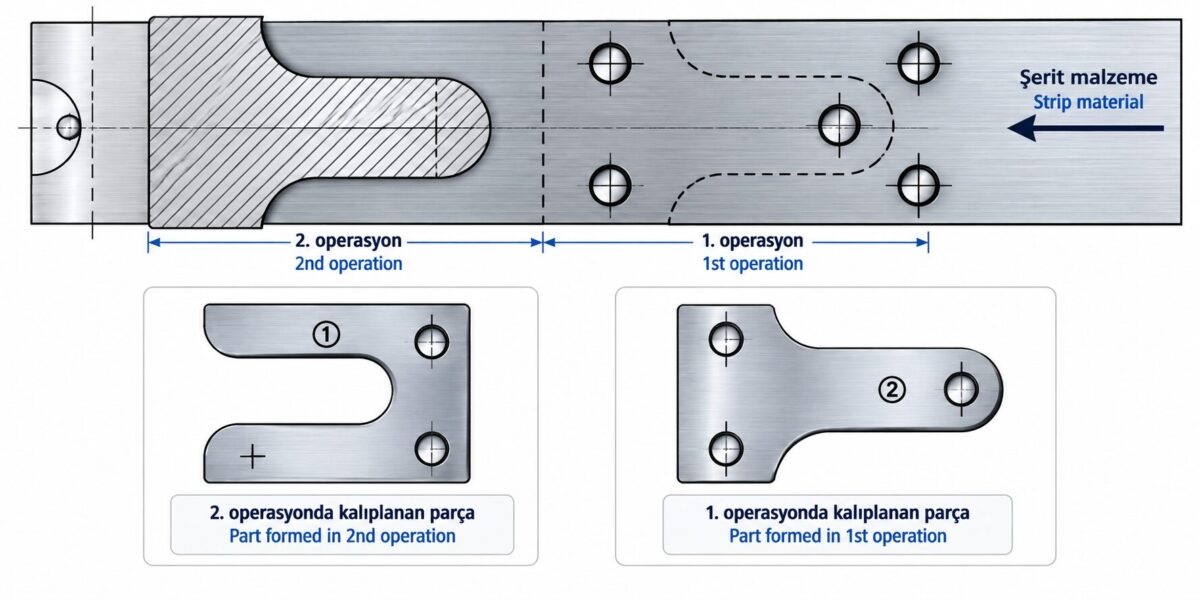
progressive die-design
şerit malzeme

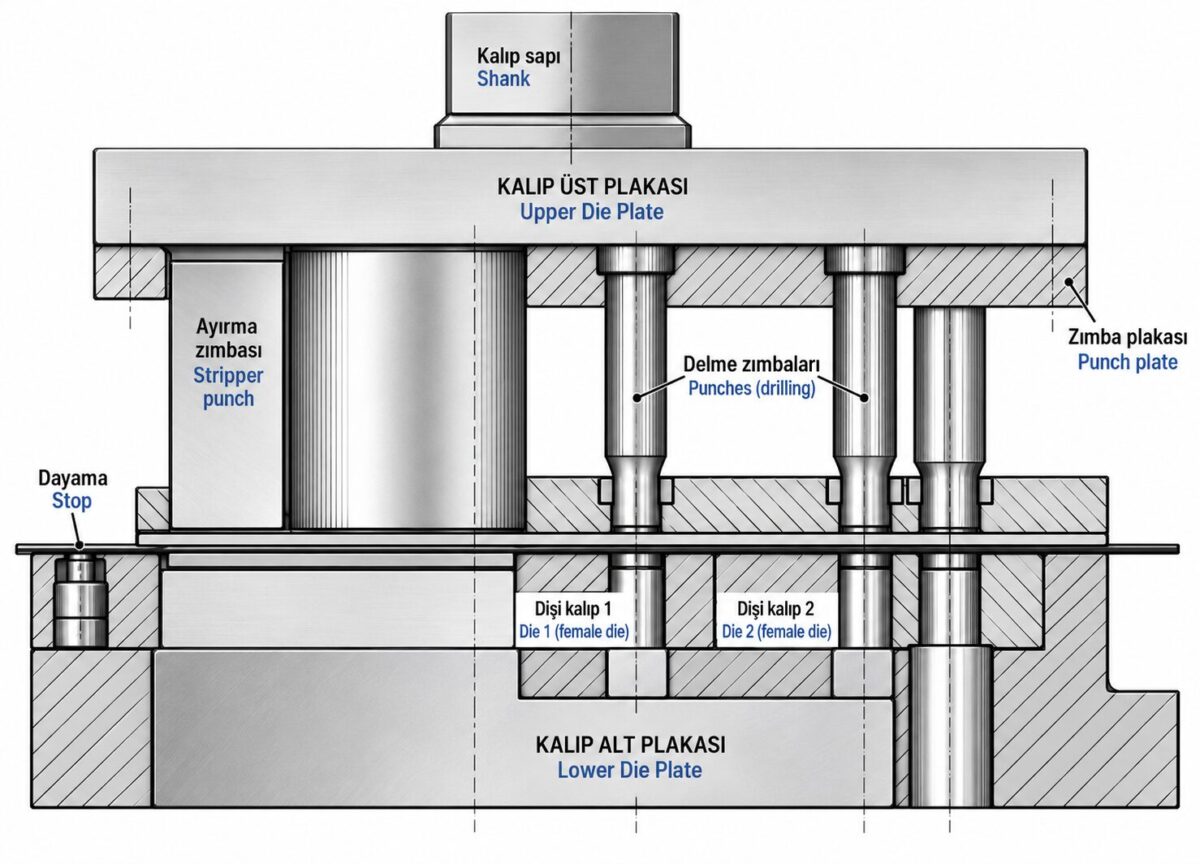
The strip material layout for the part to undergo progressive stamping operations is prepared in advance and applied directly to the female die. The figure above shows a cross-sectional view of the die illustrating the progressive stamping operation, with the strip material layout along with the produced parts shown below it.
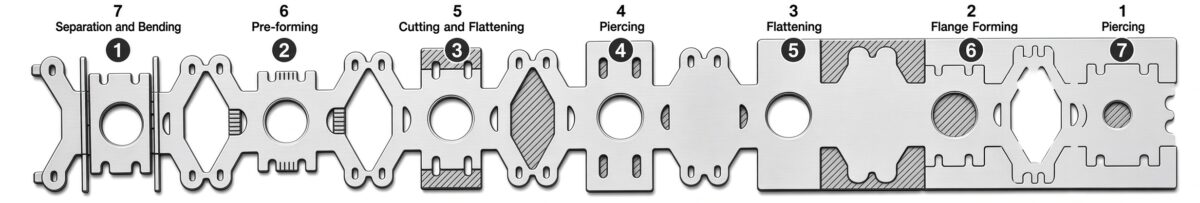
Process steps on the strip material-2
Process steps on the strip material in progressive dies
example of a part stamped with a progressive die
The stamped part and its dimensions

The figure above also shows the layout plan for the strip material for a seven-step progressive stamping operation.
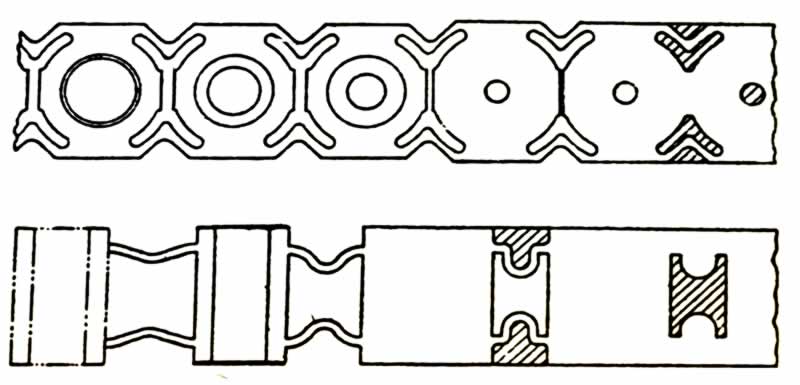
strip material die layout plan
Strip material layout plan

The figure above shows the strip material layout plans to be used in stamping two differently shaped parts.

Related Videos

Progressive stamping die

progressive die deep drawing progressive die

Deep drawing progressive die

progressive dies Precision metal stamping dies progressive stamping mold maker

Progressive stamping mold

progressive dies animation stamping tools

Stamping tools

Progressive stamping die

production with a progressive die

Electrical box stamped in progressive tool


Staged Process Sequence


Progressive dies advance the sheet strip station by station, completing a different operation at each station.

High Production Speed


By processing different stages of multiple parts in a single press stroke, progressive dies achieve very high production speeds.

Strip Feed Precision


Precisely advancing the strip to the correct station in progressive dies is critical to part quality.

Related Questions

Consecutive operations can weaken the female die; adding an idle station between them prevents this weakening and makes mounting the punches to the die easier. The tradeoff is that the die set becomes longer.

The design and construction cost of these dies is high, and this cost only comes down per part as the number of parts produced increases. For low-volume production, this high upfront cost doesn’t pay off, so a progressive die isn’t preferred.


Related Posts

Profesyonel 3d Tarayıcılar ve Kullanım Alanları Professional 3D Scanners and Their Applications How Is a Crankshaft Made How Is a Crankshaft Made Dişli Çark Üretim Yöntemleri Gear Manufacturing Methods Tel Erozyon Nedir Nasıl Çalışır? What Is Wire EDM, How Does It Work? What Is EDM, How Does It Work What Is Electrical Discharge Machining (EDM). Machining with EDM How Is a Splined Shaft Made? How Is a Splined Shaft Made? Splined Shaft Manufacturing Rondela Nasıl Yapılır How Are Washers Made laser rust removal Laser Cleaning: Removing Rust, Dirt, and Grease
Progressive Dies
Share. Facebook Twitter WhatsApp Tumblr Email Telegram Copy Link

Leave A Reply Cancel Reply


What Is Editing? What Does a Book Editor Actually Look At?
Inspection and Replacement Times for Vehicle Parts
  • Contact
  • Terms of Service
  • Privacy & Cookie Policy

Type above and press Enter to search. Press Esc to cancel.