Circular indexing operations on a milling machine using simple (direct/plain) indexing and differential indexing. Illustrated lesson with formulas, calculations, and sample applications.

To cut equal divisions on a circular part on a milling machine. (For example, this could be for producing a gear.) How much the crank must be turned is calculated based on the number of divisions to be made.
When the motion transmission ratio is 1/40 (meaning the dividing head turns 1 revolution for every 40 turns of the worm), how much the crank must be turned is calculated from the formula N = K/Z.
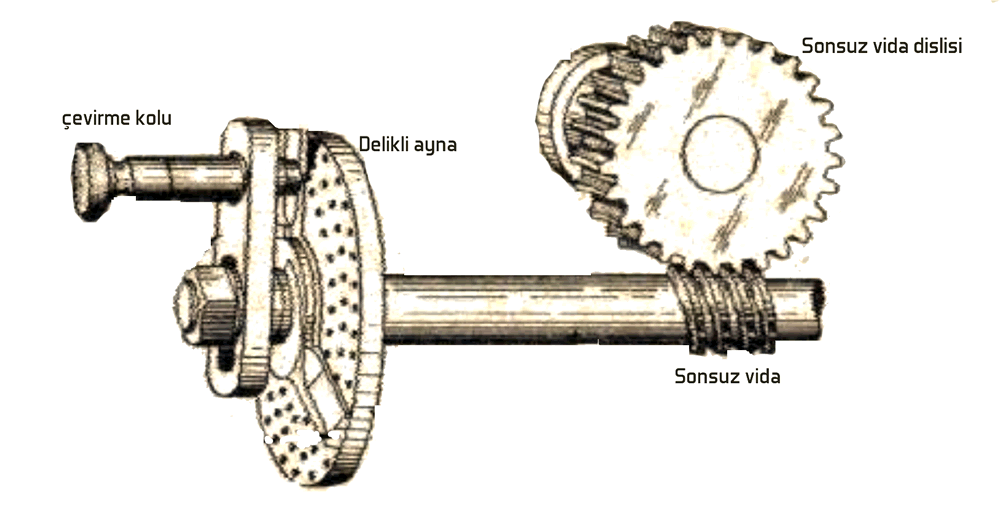
Index Plate Hole Circles (on double-sided plates)
Plate 1, side 1: 15-16-17-18-19-20
Plate 1, side 2: 21-23-27-31-33
Plate 2, side 1: 24-25-28-30-34-37-38-39-41-42-43
Plate 2, side 2: 46-47-49-51-53-54-58-59-62-66,
Simple (Direct/Plain) Indexing
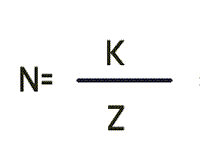
N = Number of holes or slots to turn through (on the simple-indexing plate)
K = Number of holes or slots on the simple-indexing plate (usually 24 or 36)
Z = Number of divisions to be made on the workpiece. If a gear is being made, the number of teeth
EXAMPLE
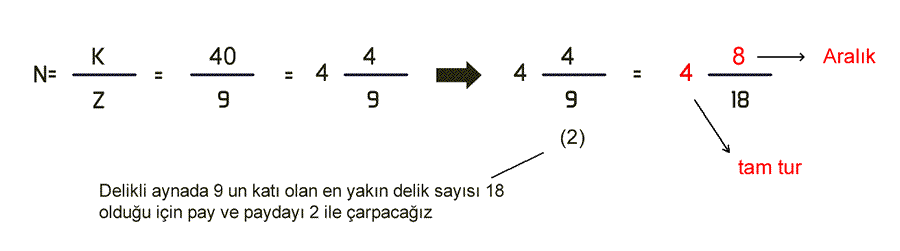
On a dividing head with a transmission ratio of 1/40, how much must the crank be turned to make 9 divisions?
SOLUTION:
Given: Z = 9 K = 40
Simple Indexing Related Videos
EXAMPLE 2
On a dividing head with a transmission ratio of 1/40, find the indexing turn for each tooth to cut a spur gear with 16 teeth.

Simple Indexing Related Videos


Differential Indexing
Divisions that can’t be made with the direct or plain indexing methods are made with differential indexing, an extended form of the indexing process. This system is used when the available index plates don’t have a suitable hole circle.

Differential indexing is achieved by combining the motion of the crank with the motion of the index plate. This coupling is done with gears fitted between the index-plate spindle (IPS) and the dividing-head spindle (DHS).
The rotary motion delivered by the crank to the dividing-head spindle is transferred to the index-plate spindle through the gears. As the crank turns, the index plate also turns, either forward or backward. This is what achieves the differential feed.
While turning the crank, the index-plate locking screw (locking pin) must not be fitted or tightened, so that the index plate is free to turn.
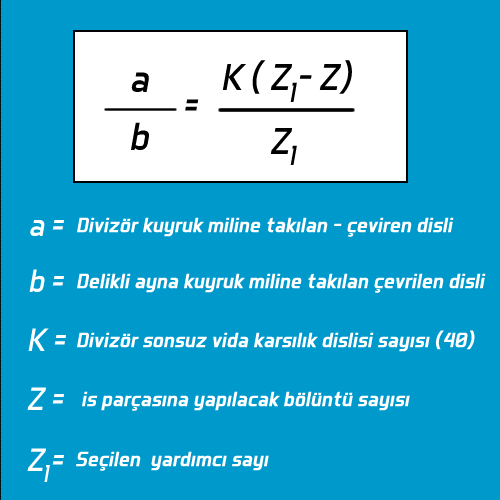
To calculate the indexing ratio, if the actual division number cannot be simplified, an approximate number is chosen instead. The difference between the indexing amounts for the actual division number and the approximate division number is called the division difference (x). By calculating the index-plate turn based on this approximate number (e.g. 21), the difference is then fed in through the change gears.
Here, the difference between the two turns is X = N – N1.
If the approximate number is chosen smaller, the index plate turns opposite to the crank; if chosen larger, it turns in the same direction as the crank.
The change gears used on a universal milling machine are found among the following tooth counts:
24-25-26-28-30-32-36-40-44-48-54-56-64-68-72-76-78-86-88-96-120-127
Differential Indexing Video Walkthrough
Sample Differential-Indexing Application on a Milling Machine
If we calculate for 71 divisions using a single change-gear setup

Related Posts