

In this article, in the Machine Technology CNC turning cycles section, we’ll cover the topic of the longitudinal turning cycle.
G90 Cylindrical ID/OD Machining Cycle (Single Pass)
With the G90 command, motion starts from the starting point with rapid traverse. After turning is performed between the given points at the specified cutting feed (F), the tool returns to the starting point with rapid traverse.
The G90 command is a modal command. Once used, it doesn’t need to be written again unless canceled. The cycle is simply repeated by changing the X value.
Once the operation is complete with the cycle command, it’s canceled with another G code from the same group (for example, with the G00 command).
The T, S, and M functions to be used in the G90 longitudinal turning cycle must be specified before the cycle is started.

G90X… Z… F…
X: End point of the first pass in the X direction
Z: The Z-axis length of the cycle
F: Tool feed rate (this is a modal G code; it can be canceled with another motion G code once the passes are complete)
EXAMPLE
G90 X36 Z-20 F0.1
X32
X28
X25
Example of the G90 Cylindrical ID/OD Machining Cycle
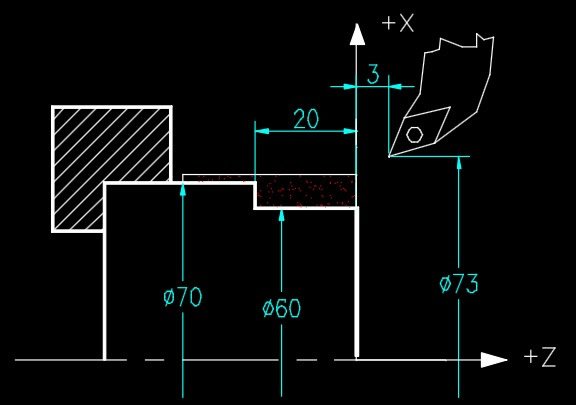
Machining program for the part shown above, using tool no. 1, with a constant cutting speed of
150 m/min and a feed rate of F0.18 mm/rev:
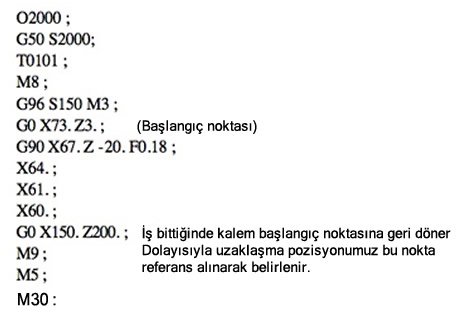
Using the G90 Code for Internal Diameter Machining

Let’s give another example, this time about how the G90 code can be used for boring operations.
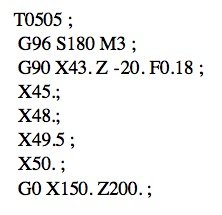
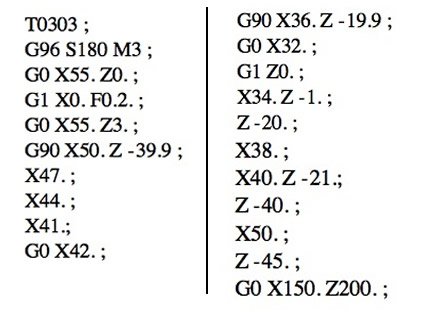
Another Example of the G90 Longitudinal Turning Cycle
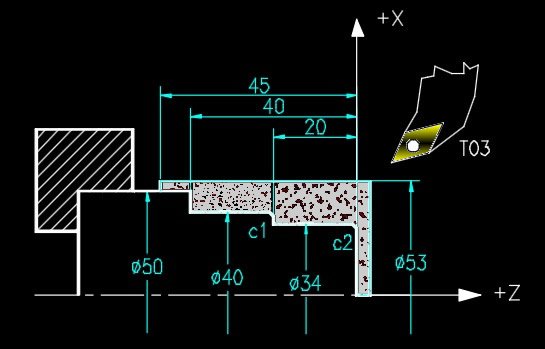
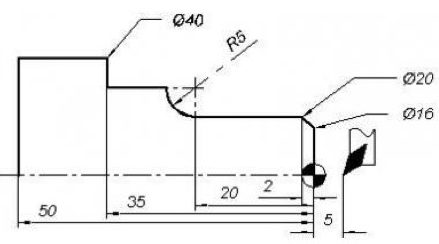
The part given above is provided as a somewhat more detailed example. Try to work out from the code how the G90 code can be used for a part like this, and how the part would be machined.
G90 Fixed Cycle Convenience
The G90 cycle automates repeated cylindrical turning passes with a single line of code.
G71 Roughing Efficiency
The G71 cycle lets you program roughing on complex-profile parts with just a few lines of code.
G70 Finishing Pass Accuracy
The G70 cycle is used to finish the profile defined by G71 to its final dimensions with a smooth surface.
G71 OD Roughing Cycle (Turning Parallel to the Axis)
The G71 stock removal cycle is used to machine shapes whose profile varies monotonically along both the X axis and the Z axis.
Once the finishing profile is defined in the program, the roughing pass movements are performed automatically. A finishing allowance of U2 is left on the X axis, and W on the Z axis.
After the G71 cycle, this remaining finishing allowance is also removed by the G70 cycle to complete the operation.

Description of the Cycle:
G71 U(1)… R…
G71 P… Q… U(2)…W… F…
U(1): Depth of cut on diameter for each pass
R: Retraction amount after each pass
P: Sequence number of the first block of the finishing profile
Q: Sequence number of the last block of the finishing profile
U(2): Finishing allowance on diameter
W: Finishing allowance on the face
F: Cutting feed rate during the cycle
G70 – FINISHING PASS CYCLE
It’s used to remove the finishing allowance left behind by the G71 – G72 – G73 cycles.

G70 P… Q…
P: Sequence number of the first block of the finishing profile
Q: Sequence number of the last block of the finishing profile
G70 Example Program:


Related Questions
Being modal means that once the command is written, it doesn’t need to be written again until it’s canceled. This lets the operator repeat the same turning cycle over and over just by changing the X value, which shortens the program.
Lines written one after another in the program, changing only the X value each time, turn a different diameter each time using the same Z and F settings. This allows a stepped machining process without requiring the operator to rewrite all the parameters for every pass.
Related Posts
 CNC Lathe Programming Examples
 CNC Facing Cycle – G94-G72-G70
 G74 CNC Peck Drilling Cycle Explained
 What Is iMachining, Advanced CAD/CAM CNC Machining Technology
 CNC G Code List and Meanings (Beginner’s Guide)
 Fanuc CNC Error Codes – Fanuc Fault Codes
 Powering On a Fanuc CNC Lathe. How Is a CNC Lathe Powered On
 CNC Milling Programming Examples