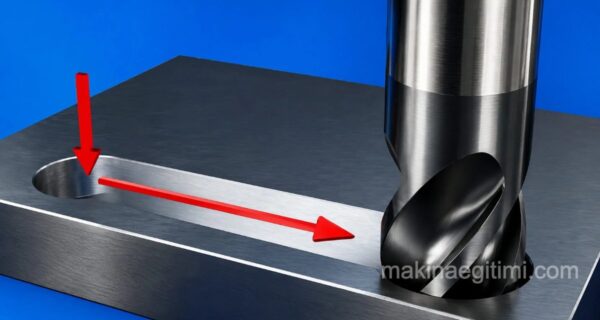
GROOVE: Cylindrical recesses formed on the face, inner, and outer surfaces of cylindrical parts on a lathe are called grooves. In practice, three types of grooves are used very often. a) Square groove b) Round groove c) V groove
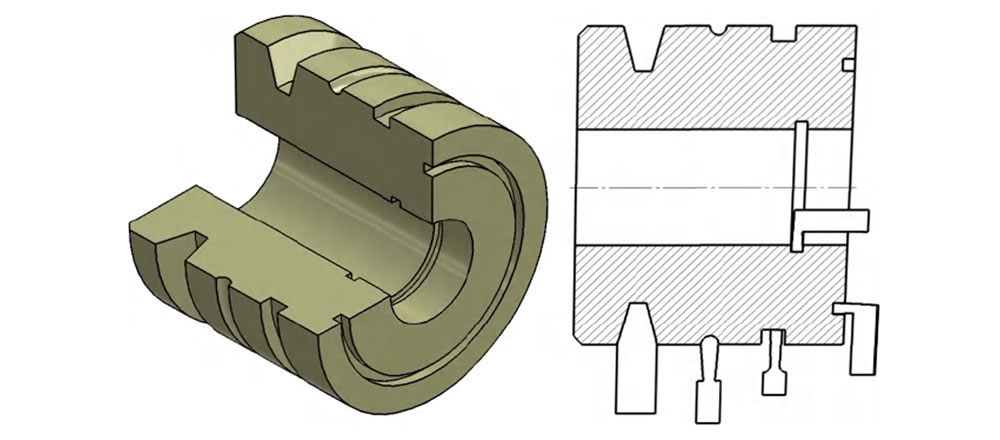
Why Is Groove Turning Done?

A grinding relief groove is cut at the base of steps on stepped shafts. (1) When cutting a thread on a lathe, a groove is cut at the end of the thread so the threading tool can run off smoothly. (2)

Grooves are cut into pulleys for V-type and round belts. (Above)
To fix the position of bearings, a retaining ring groove is cut inside bores and on the outer surfaces of cylindrical parts. (Image above) Click here to watch the video animation
On machine parts that rotate against one another, oil grooves are also cut as a helical channel using a round-nose grooving tool.
In assembly operations, a groove is cut so that a threaded part’s shoulder seats properly against the face of another part.
A groove is cut to fit o-rings, which are sealing elements.
At the locations on machines where bearings are fitted, a groove is cut into the face of the cylindrical part on the bearing cap so a sealing element can be fitted.
Grooving Tools
The cutting tool used to cut grooves on a lathe is called a grooving tool (parting-off tool). There are both types ground from HSS steel and ready-made carbide-insert tools sold commercially.
Grinding the Grooving Tool
Mounting the Grooving Tool
The grooving tool must be mounted at center height. (If mounted too high, it dulls quickly and won’t cut. If mounted too low, it will tend to dig into the work and the tool will break.) Depending on the position and angle of the groove, it can be mounted on the tool post either perpendicular to the workpiece axis or at an angle.
Grooving tools generally have a narrow profile. Choosing one narrower than the width of the groove makes it easier to achieve precise dimensions.
Grooving Tool Geometry
Grooving (parting) tools have a thin, elongated cutting-edge geometry to allow cutting narrow and deep grooves.
Low Feed Rate
Low feed rates are generally preferred in groove turning to prevent tool breakage.
O-Ring Groove Application
Groove turning is often used to cut precisely dimensioned grooves that will seat o-ring gaskets.
Steps for Groove Turning
1- Mount the grooving or parting tool to be used properly.
2- Zero out the grooving tool against the surface, both transversely and longitudinally, on the micrometer collar.
3- Set the machine to the appropriate speed for cutting the groove.
4- Centering the tool on the groove to be cut, cut the groove until you reach the desired diameter.
5- If the groove needs to be widened, repeat the operation by shifting right and left (not while inside the groove).
6- To prevent the tool from jamming in deep grooves, cut the groove slightly wider than the tool.
7- Deburr the corners with a file before handing off the finished part
Groove Turning Practice Workpieces
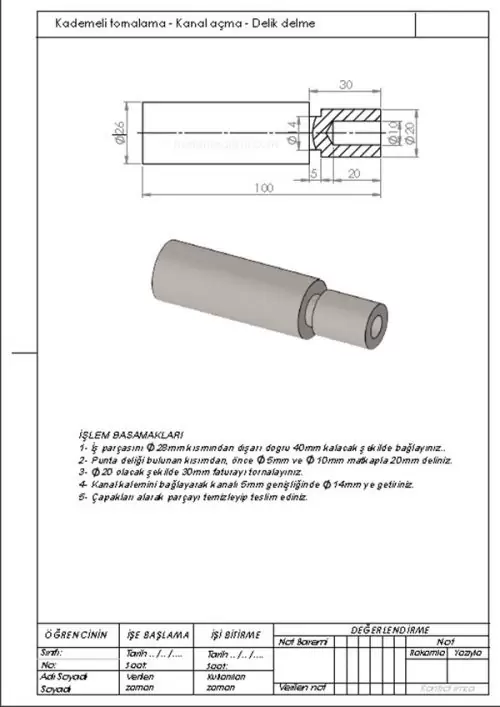
Stepped turning-groove cutting-drilling practice workpiece (exercise) DOWNLOAD PDF

Stepped turning and groove cutting
Practice workpiece (exercise) DOWNLOAD PDF
Related Questions
During grinding, it’s difficult for the grinding wheel to seat fully into the corner of a step, and a rough transition can remain at the corner. The cut groove gives the wheel room to work comfortably in this corner, ensuring a clean and sharp step transition.
Since an o-ring is a flexible material, it can’t stay fixed on a flat surface and could slip out of place. The cut groove keeps the o-ring in place, maintaining a permanent seal between the two parts.
Related Posts