
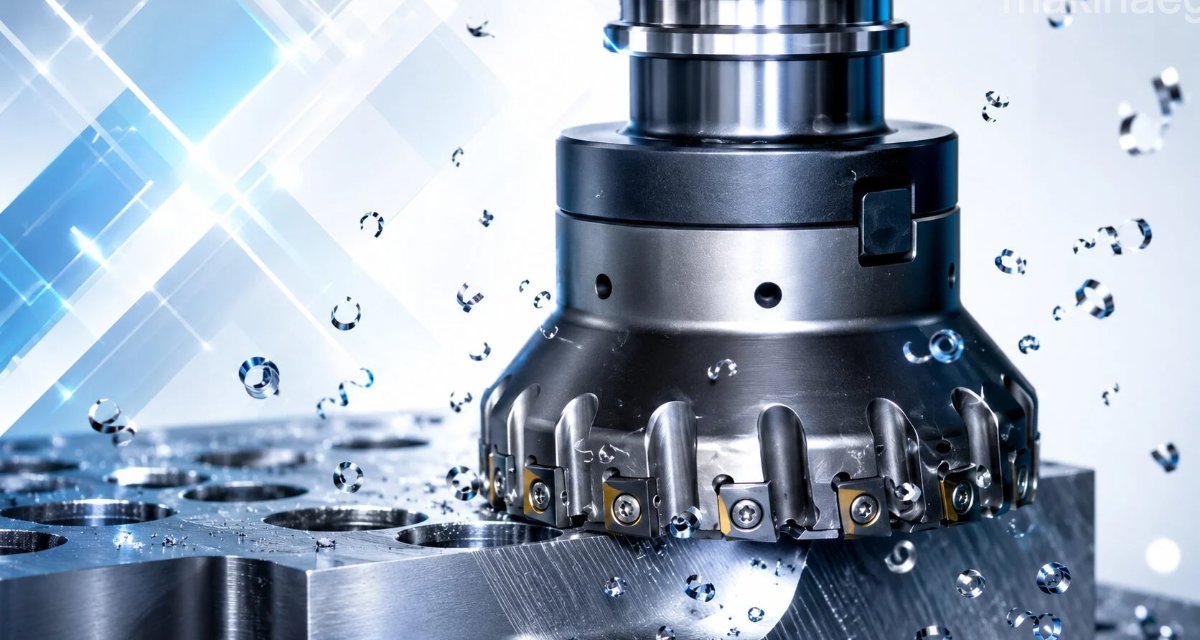
This article is about machine manufacturing. We’ll focus on why the cutting tool wears during milling, and how tool wear can be minimized or eliminated.
Chipped cutting edges and constantly varying chip thicknesses subject the cutting edges of the milling cutter to high mechanical and thermal loading. These are the primary causes of cutting-edge wear and the resulting shorter tool life.
Types of Cutting Tool Wear
Flank Wear
This is the normal form of wear at the end of a tool’s useful life. If wear occurs quickly, this can be prevented by choosing a wear-resistant carbide grade for the insert and, if needed, reducing cutting speed and increasing the feed rate.
Crater Wear
This can occur when machining steels. If crater wear becomes very severe, the cutting inserts can break. In cases of very severe crater wear, it’s also recommended to reduce the cutting speed and choose a more wear-resistant carbide grade.
Transverse Cracks
These are fatigue cracks that form along the cutting edges, caused by high impact loading (stress) as the cutting edges engage the material, and by continuously varying cutting forces. During conventional (up) milling, the risk of the cutting edges breaking increases.
Comb Cracks
These arise from temperature fluctuations during interrupted cutting perpendicular to the cutting edges. These cracks can be prevented by using a smaller-diameter milling cutter, reducing the cutting speed and feed per tooth, and by choosing a tougher (more cohesive) carbide grade. Coolant should never be used under any circumstances.
Chipping and Flaking
This results from high temperature fluctuations. Choosing a tougher carbide grade, along with honing the cutting edges to round off their edges, and stabilization, can provide emergency relief in this regard.
Built-Up Edge
This occurs if chips adhere to and weld onto the cutting edges at very low temperatures. A built-up edge lowers surface quality and increases power requirements. Increasing feed rate and cutting speed, and improving chip flow with a positive rake angle, can counteract the formation of a built-up edge.
Deformation of the Cutting Edges
This occurs due to very high mechanical stresses. Reducing cutting parameters and choosing a harder carbide grade can eliminate this problem.
Flank Wear
Flank wear results from the tool rubbing against the material and directly affects surface quality.
Crater Wear
Crater wear is a pit that forms on the tool surface due to high temperature and is typically associated with high cutting speed.
Effect of Cutting Parameters
An incorrectly chosen cutting speed and feed rate can cause milling tools to wear far faster than expected.
Related Questions
An incorrect cutting speed and feed rate can cause milling tools to wear far faster than expected.
Flank wear results from the tool rubbing against the material and directly affects surface quality.
Crater wear is a pit that forms on the tool surface due to high temperature and is typically associated with high cutting speed.
Related Posts
 Helical Gear Geometry and Strength Calculation
 Cutting Tool Wear Types and Causes of Wear
 The Relationship Between Cutting Tools and Surface Roughness
 Chip Types and Forms in Machining
 The Software Mechanical Engineers Use the Most
 Forces Acting on the Crankshaft. Crankshaft Material
 Chip Control and Chip Breakers in Metal Machining
 Forces Acting on the Piston and Piston Material