Close Menu
  • MAKİNELER ve İMALAT
    • Tools & Equipment
    • Computer-Aided Drawing
    • CAD/CAM Education
    • CNC Machine Programming
    • Casting Technologies
    • Electrical & Electronics Technologies
    • Hydraulics & Pneumatics
    • Manufacturing Processes
    • Manufacturing Technologies
    • Occupational Safety
    • Mold & Die Design
    • Solid Modeling
    • Welding Technology
    • Machine Elements
    • Mechanical Trade Drawing
    • Materials Science
    • Automotive & Vehicle Technologies
    • Robotics Technologies
    • Health Technologies
    • Defense & Aerospace Technologies
    • Descriptive Geometry
    • Technical Drawing
    • Software & Hardware Technologies
    • Innovative Manufacturing Methods
  • TEKNOLOJİ ve YAŞAM
    • OTOMOBİLLER ve TAŞIT
      • Vehicle & Engine Knowledge
      • Safe Driving
      • Sürüş Destek Sistemleri
    • Genel Kültür
      • Movies & TV Shows
      • Görsel ve Grafik Sanat
      • Books & Literature
      • Music
      • Sports
      • History
      • History of Technology
    • GÜNDELİK YAŞAM TEKNOLOJİLERİ
    • Hobbies & Entertainment
    • Internet Technologies
    • Health
    • Mobile Technologies
Makine Eğitimi
  • Machines & Manufacturing
    Machine Elements
    Hydraulics & Pneumatics
    Technical Drawing
    Computer-Aided Design & Manufacturing
    Basic Manufacturing Processes
    Manufacturing Processes
    Industry Technologies
    Other Technical Courses
    Motion & Power Transmission
    Simple Machines
    Chains & Sprockets
    Shafts & Journals
    Gears
    Cams
    Couplings
    Belts & Pulleys
    Springs
    Bearings
    Keys
    Fastening Joining
    Retaining Rings
    Screws, Bolts & Nuts
    Cotter Pins
    Flanges
    Welding
    Rivets
    Pins & Bolts
    Washers
    Calculators
    Gear Ratio Calculator
    Spring Constant Calculator
    Belt Pulley Ratio Calculator
    Other Machine Elements
    Slides & Linear Guides
    Brakes
    Flywheels
    Clamps
    Shock Absorbers
    Gaskets & O-Rings
    Seals & Sealing Elements
    Hydraulics
    Introduction to Hydraulics & Principles
    Hydraulic Systems & Applications
    Accumulators
    Filters
    Motors
    Pumps
    Valves
    Pneumatics
    Introduction to Pneumatics & Principles
    Pneumatic Systems & Applications
    Pneumatic Circuit Components
    Valves
    Cylinders
    Silencers
    Motors
    Compressors
    Dryers
    Conditioning Units
    Common Topics & Maintenance
    Hydraulic & Pneumatic Maintenance
    Study Notes, Exams & Tests
    Technical Drawing
    Introduction to Technical Drawing
    Geometric Drawings
    Perspective & Projection
    Orthographic Views
    Dimensioning
    Sectioning
    Assembly & Detail Drawings
    Tolerances
    Surface Finish Symbols
    Mechanical Engineering Drawing
    Screws, Bolts & Nuts
    Pulley Drawings
    Gear Drawings
    Shafts & Journals
    Bearing Drawings
    Pins & Bolts
    Spring Drawings
    Welds in Technical Drawing
    Washers
    Cotter Pins
    Technical Drawing Exercises
    Mechanical Drawing Exercises
    Gear Exercises
    View Extraction Exercises
    Pulley Exercises
    Pin & Bolt Exercises
    Threaded Fastening Exercises
    Descriptive Geometry
    Computer-Aided Drawing
    AutoCAD Drawing Lessons
    Solid Modeling & Animation
    Solid Model Drawing Files
    Solid Model Assembly Examples
    Solid Model Drawing Lessons
    3D CAD Software Reviews
    Solid Modeling Exercises
    CNC Programming
    CAM
    Measurement & Inspection
    Dial Indicators
    Calipers
    Gauges
    Micrometers
    Materials Science
    Steels
    Cast Iron
    Aluminum
    Plastics
    Material Testing & Hardness Measurement
    Occupational Safety
    Workshop Safety
    Safety When Working With Electricity
    Machine Safety Rules
    Hand Operations
    Filing
    Marking
    Cutting Operations
    Reaming
    Tapping
    Threading With a Die
    Drill Bit Sharpening
    Working With Machines
    Basic Turning Operations
    Basic Milling Operations
    Shaper Machine
    Machining
    Turning
    Milling
    Grinding
    Innovative Manufacturing Methods
    EDM (Electrical Discharge Machining)
    Laser Machining
    Waterjet Machining
    3D Printing
    3D Scanners
    Welding
    Rolling
    Casting
    Mold & Die Design
    Mechanical & Hydraulic Presses
    Blanking & Piercing Dies
    Bending Dies
    Drawing Dies
    Plastic Injection Molds
    Extrusion Dies
    Compound Dies
    Progressive Dies
    Blow Molds
    Spinning Dies
    Spray Molds
    Manufacturing of Machine Parts
    Automotive & Vehicle Technologies
    Motor Vehicle Manufacturing
    Raw Material Production
    History of Technology
    Health & Medical Technologies
    Defense & Aerospace
    Robotics Technologies
    Software & Hardware Technologies
    Mechanics - Strength of Materials
    Physics Topics
  • Technology & Life
    Hobbies & Entertainment
    Sports
    Music
    Vehicle & Engine Knowledge
    Vehicle Maintenance & Repair
    Safe Driving
    Driver Assistance Systems
    History
    Movies & TV Shows
    Books & Literature
    Computers & Internet
    Computer Tips
    Software Reviews
    Hardware & Peripherals
    Practical & Safe Internet Use
    Visual & Graphic Art
    Mobile Technologies
    Travel
    Science
    Health
    First Aid Knowledge
    Everyday Technologies
Makine Eğitimi
Home»Mechanical Engineering Academic Knowledge»Chip Types and Forms in Machining
30 August 2026

Chip Types and Forms in Machining

talaşlı imalatta talaş tipleri

Formation of Chips

As the tool advances toward the workpiece during machining, the metal ahead of it is compressed. When the compression exceeds the material’s limit, the metal separates from the workpiece and flows plastically in the form of a chip (shear deformation).

  • Formation of Chips
  • Types of Chips
  • Related Questions
chip types in machining

Due to primary cutting, the metal flow occurs along the shear plane. The shear plane extends upward at an angle from the uncut surface ahead of the tool. The value of the shear angle depends on the type of material and the cutting conditions (tool angle, cutting speed, etc.). When the shear angle is small, the shear path is long, the chips are thick, and the cutting force is high, and vice versa. 

As the chip slides along the face of the tool tip, secondary cutting occurs due to friction. This friction raises the temperature of the machining process, causing the chips to overheat. 

Continuous Chip


A continuous chip usually forms as a long ribbon when ductile materials are machined at high cutting speeds.

Discontinuous (Segmented) Chip


A discontinuous chip forms as small segments when machining brittle materials such as cast iron.

Built-up Edge Chip


A built-up edge, which forms at low cutting speeds, can stick to the tool tip and negatively affect surface quality.

Types of Chips

The types of chips formed during the machining of metals are;

  • Segmented chip
  • Continuous chip
  • Built-up edge continuous chips

Segmented (Discontinuous) Chips

Segmented chips generally occur when machining brittle metals such as brass, bronze, or cast iron.

In general, segmented chips are the result of the following machining conditions;
Low feed rate;
High cutting speed;
High tool-chip friction;
Significant depth of cut
Low rake angle.

  • Low feed rate;
  • Low rake angle;
  • High cutting speed;
  • High tool-chip friction;
  • Significant depth of cut.

Segmented chips provide a clean surface finish, easy chip disposal, longer tool life, and reduced power consumption in brittle metals. In the case of ductile metals, segmented chips generally cause poor surface quality and shorter tool life.

Continuous Chips

turning continuous chip

Continuous chips generally form when machining malleable metals such as steel, copper, or aluminum at high cutting speeds. During machining, the temperature between the tool tip and the ductile workpiece rises. Each layer of removed metal welds onto the previous layer, forming a long, continuous chip flow.

Continuous chips form under the following machining conditions;
Small depth of cut,
Large rake angle;
High cutting speed;
Low tool-chip friction (use of lubricants or coolants);
Sharp cutting edge.

Continuous chips provide a clean surface finish, longer tool life, and reduced power consumption. On the other hand, disposing of this type of chip is difficult. Chip breakers must be used to improve disposal conditions.  

Built-Up Edge (BUE) Continuous Chips
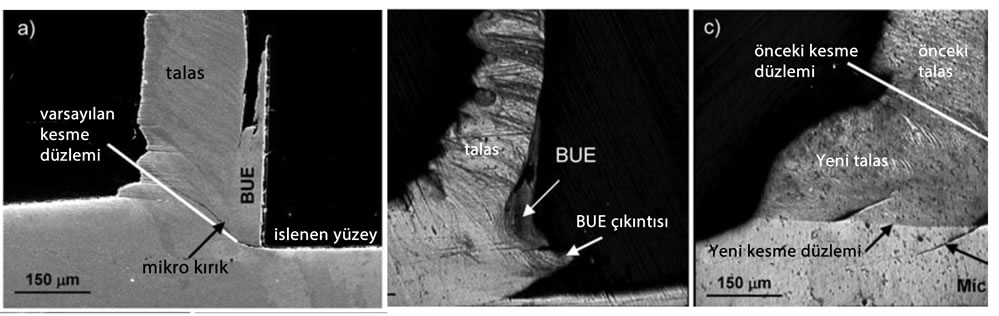
bue built-up edge continuous chip type

Continuous chip formation with BUE (Built up Edge) results from high friction between the tool and the chip when machining ductile metals. Under these conditions, some chip particles tend to adhere to the cutting tool. The adhered material continues to build up, forming a new cutting edge, until it separates from the tool. During separation, the built-up material adheres to both the chip and the workpiece surface, causing poor surface quality. Another name for BUE formation is “chip welding“.

Continuous chips with a built-up edge occur under the following conditions:
Low rake angle;
Low cutting speed;
High friction forces;
High feed.

Since continuous chips with BUE adversely affect tool life, increase power consumption, and cause poor surface quality, preventing them is very important. Measures such as reducing friction through the use of lubricants, preventing metal-to-metal contact through tool coatings, and lowering the temperature using cutting fluids have a positive effect on preventing chip welding. 

Related Questions

This difference comes from the structure of the material being machined. Ductile materials produce a long, continuous ribbon of chip when cut at high speed, while brittle materials such as cast iron break into small segments during cutting.

At a small shear angle, the path followed by the chip lengthens and the chip becomes thicker. Since cutting a thicker chip creates more resistance, the cutting force exerted by the tool also increases.

Related Posts

Forces Acting on the Piston and Piston Material Forces Acting on the Piston and Piston Material Forces Acting on the Crankshaft and Crankshaft Material Forces Acting on the Crankshaft. Crankshaft Material Cutting Tool Wear Types and Causes of Wear chip breaking in turning Chip Control and Chip Breakers in Metal Machining The Relationship Between Cutting Tools and Surface Roughness The Relationship Between Cutting Tools and Surface Roughness Helis Dişli Geometrisi ve Mukavemet Hesabı Helical Gear Geometry and Strength Calculation The software mechanical engineers use the most The Software Mechanical Engineers Use the Most Frezelemede Kesici Takım Aşınma Sebepleri Causes of Cutting Tool Wear in Milling
Share. Facebook Twitter WhatsApp Tumblr Email Telegram Copy Link

Leave A Reply Cancel Reply

What Is a Diesel Particulate Filter Fault. How Is It Detected
Why Does an Engine Misfire? Engine Misfire Problem
  • Contact
  • Terms of Service
  • Privacy & Cookie Policy

Type above and press Enter to search. Press Esc to cancel.