
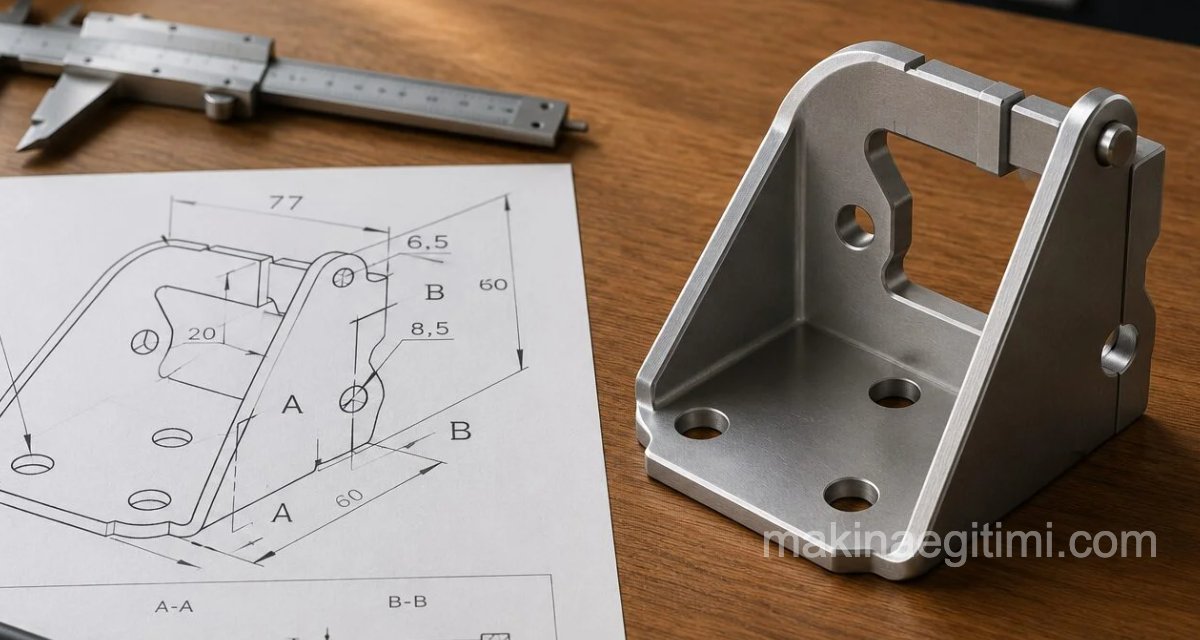
Bending is generally the process of deforming sheet or strip material around an axis. Sheet materials are subjected to bending within their plastic deformation limits. Once the applied bending force is removed from the part, it retains its permanent shape. Compressive stress develops on the inner surface of a part being bent, and tensile stress develops on the outer surface.
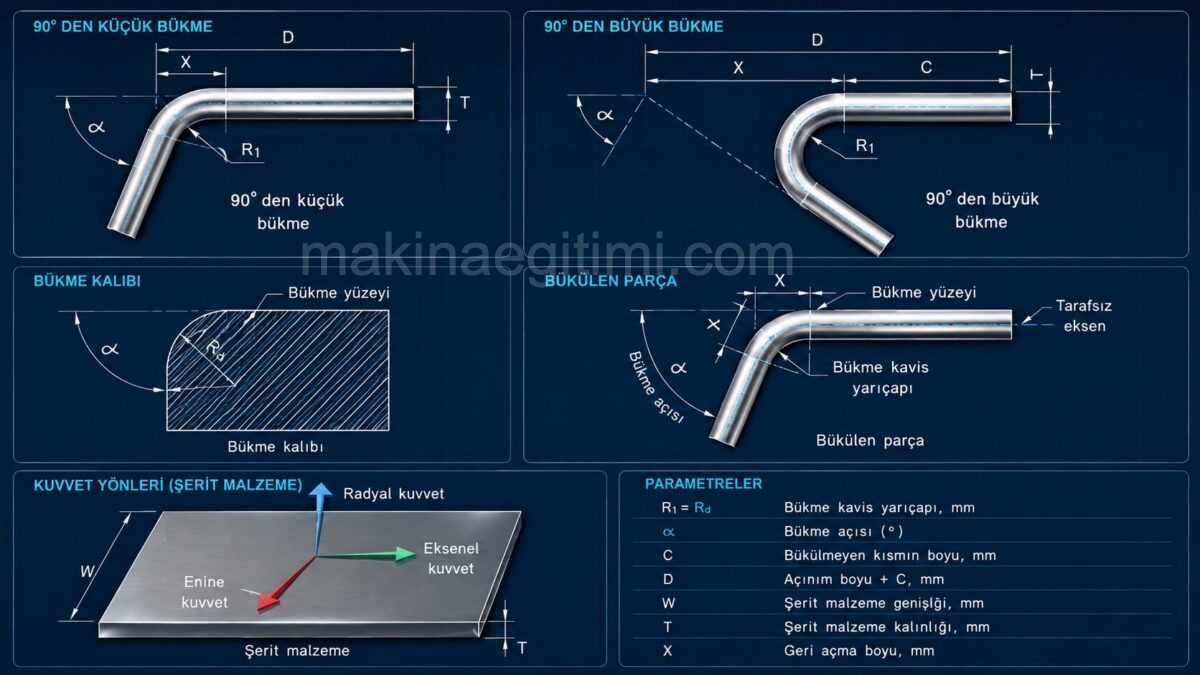
Along with this, elongation occurs on the outer surface and shortening occurs on the inner surface. The location where tensile and compressive stress are zero (0) lies on the neutral axis of the bent part. The figure above shows the deformation occurring on a bent part, the bend radius, the bend angle, and the neutral axis.
Bend Radius
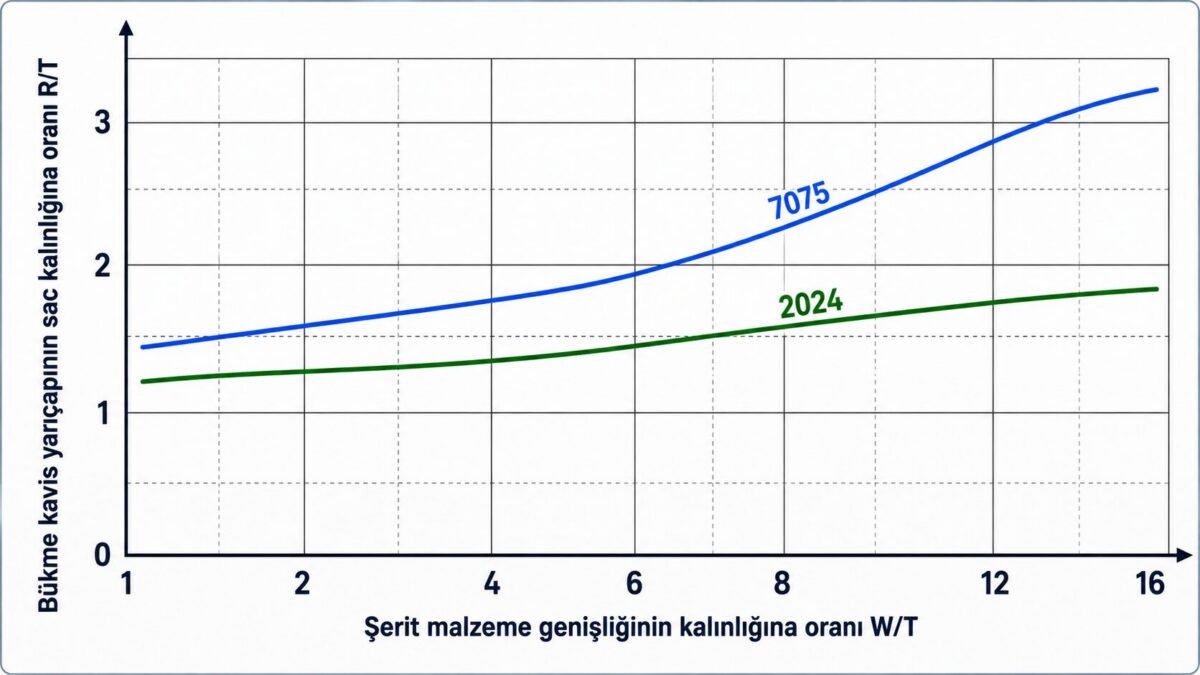
The bend radius varies depending on the type and thickness of the sheet material. Generally, for materials that have undergone normal annealing, the bend radius (R1) is taken equal to the sheet material’s thickness. Sometimes the bend radius can also be taken as half the sheet thickness (T/2). However, this depends on the sheet material’s thickness and rolling direction. The bend width also has an effect.
When the bend radius is 8 or more times the sheet thickness, the width of the bent part affects the minimum bend radius.
Strip Material Grain Angle
When bending sheet or strip material in the rolling direction, the bend radius (R1) is limited. To prevent faulty bending, strip material is cut at a certain grain angle relative to the sheet’s rolling direction. The strip material’s grain angle φ, relative to the rolling direction, can be increased. Bending perpendicular to the rolling direction is generally the most common approach, but this may not be possible with some materials or with small-radius bends.
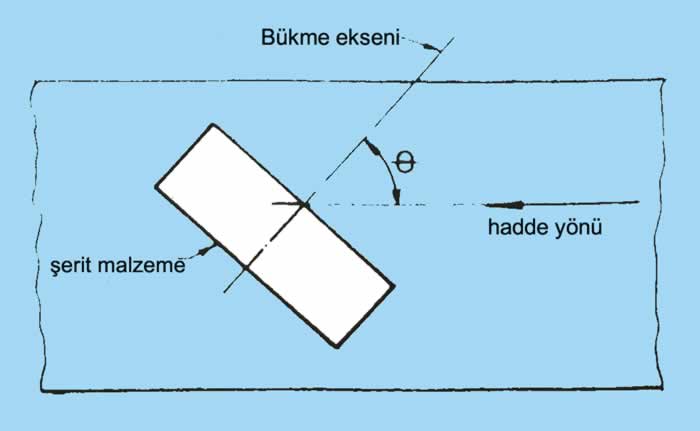
The strip material’s grain angle is shown in the figure above.

Strip material grain angle values by material type
Neutral Axis
When sheet material is forced to bend, tensile stresses form on the outer surfaces and compressive stresses form on the inner surfaces. Shortening occurs on the surface where compressive stress is present, and elongation occurs on the surface where tensile stress is present. The axis that lies between the compressive and tensile stresses, and that undergoes neither elongation nor shortening, is called the neutral axis.

The figure above shows a part undergoing bending, along with the elongation, shortening, and neutral axis for this part.

Depending on the bend radius, the neutral axis shifts somewhat toward the bend’s curved surface. The amount and characteristics of this shift are shown in the figure above.
The neutral axis of a sheet material undergoing bending generally shifts toward the inner surface by about 4/10 of the sheet material’s thickness. This amount of shift can be explained as follows.
- If the sheet material thickness is constant and the bend radius decreases, the neutral axis shifts toward the inner surface.
- If the bend radius is constant and the sheet material thickness increases, the neutral axis shifts toward the inner surface.
- If the sheet material thickness and bend radius are constant and the bend angle increases, the neutral axis shifts toward the inner surface.
Amount of Springback
You can find detailed information about springback in bending dies, and how to calculate the amount of springback, on the page linked below.
Related Post Calculating the Amount of Springback in Bending Dies
Calculating the amount of springback in bending dies and compensating for springback. What can be done to eliminate springback in bend forming.
Video on Bending Die Design
Related Posts
Calculating the Amount of Springback in Bending Dies  Mold Making With the Selective Laser System
 Calculating the Cutting Force in Dies
 Spinning Mandrels and Spinning Machines
 Drawing Defects in Drawing Dies and How to Resolve Them
 Carbide Dies and Punches in Drawing Dies
 Compression Molds and Their Types
 Drawer Rail Piercing Die Assembly and Detail Drawings