
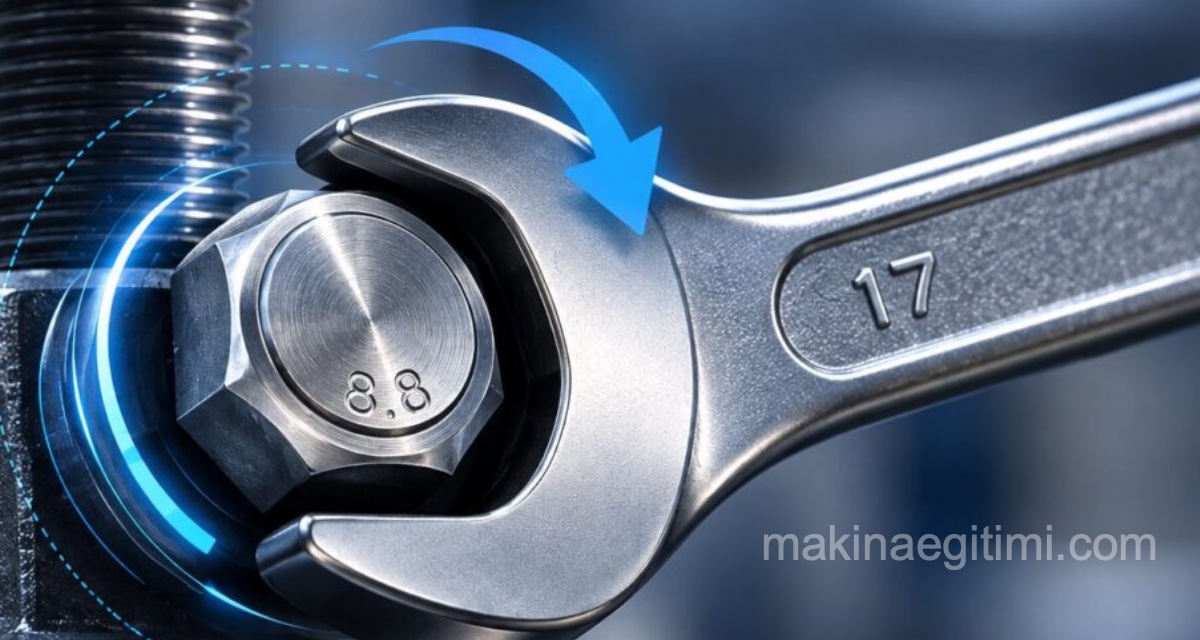
Tightening a bolt to the correct torque matters far more than it looks: an under-tightened bolt loosens under vibration, while an over-tightened one can snap or crush the threads/part. The correct tightening torque depends on the bolt’s diameter, the desired preload (clamping) force, and the surface’s friction condition. With the interactive calculator below, you can enter these three values to instantly find the required tightening torque, and watch the tightening process with a live animation.
Why Does Tightening Torque Matter?
When a bolt is tightened, it actually stretches slightly, and this stretch creates a preload (clamping) force that presses the two parts together. This force keeps the joint from loosening during operation and helps it resist vibration.
If the tightening torque is too low, insufficient preload develops and the joint loosens over time; if it’s too high, the bolt can be stretched beyond its yield point — permanently elongating it, stripping the threads, or breaking the bolt.
How Is Tightening Torque Calculated?
Tightening torque is calculated with the formula T = K × F × D. Here, T is the tightening torque (Nm), F is the desired preload force (N), D is the bolt’s nominal diameter (mm, converted to meters in the calculation), and K is the torque coefficient (friction coefficient). K is a dimensionless number that depends heavily on surface/lubrication condition. Typically around 0.20 for dry steel-on-steel contact, but much lower (around 0.13-0.17) for lubricated or anti-seize coated surfaces.
For example, to tighten an M10 (10 mm) bolt on a dry surface (K=0.20) to a preload force of 15 kN: T = 0.20 × 15,000 × 10 / 1000 = 30 Nm. If the same bolt is tightened on an anti-seize coated surface (K=0.13), the torque required for the same preload force drops to just 19.5 Nm. Showing how much the torque coefficient affects the result.
Why Is the Torque Coefficient (K) So Variable?
Most of the applied torque (typically 80-90%) is actually spent overcoming friction on the thread surfaces and under the bolt head, not stretching the bolt. Only a small portion converts into actual preload force.
That’s why surface condition (dry, lubricated, galvanized, anti-seize coated) directly affects the K value and thus the required torque. Even when targeting the same preload force, a lubricated bolt reaches the same result with far less torque than a dry one. Which is why using the manufacturer-specified K value (or torque table) is critical for correct assembly.
Bolt Torque Calculator
Enter the bolt diameter and desired preload force into the tool below, then select the surface/lubrication condition from the list to get an automatic torque coefficient suggestion (you can also edit the K value manually). The required tightening torque is calculated instantly, and the tightening process is animated visually.
Torque is calculated as T = K × F × D. The torque coefficient (K) varies widely with surface/lubrication condition; the values above are approximate, for educational reference only — in real applications, use the value provided by the fastener manufacturer.
Applications Where Correct Tightening Torque Matters
- Cylinder head bolts: insufficient torque prevents the gasket from sealing properly, while excessive torque can damage the gasket surface.
- Wheel lug bolts: wheel bolts not tightened evenly and to the correct torque can loosen while driving, creating a serious safety risk.
- Structural steel connections: insufficient preload in load-bearing connections can prevent the joint from carrying its design load.
- Precision electronic/optical assemblies: excessive torque can deform or crack delicate components.
Frequently Asked Questions
The most accurate value comes from the bolt/nut manufacturer’s torque table or technical documentation. If a general estimate is needed, typical values are around 0.20 for dry steel-on-steel contact, 0.17 for lightly lubricated surfaces, and 0.13 for anti-seize or PTFE-coated surfaces — but critical applications should always use the manufacturer’s data.
Over-tightening risks stretching the bolt beyond its yield point — permanently elongating it (plastic deformation) so the preload force ends up lower than expected, or even breaking the bolt or stripping the threads. This is why using a torque wrench, especially on critical joints, is far safer than tightening “as much as you can.”
No — the relationship between torque and preload force depends on the torque coefficient (K), and since K depends on friction, it’s affected by surface roughness, lubrication, corrosion, and even repeated assembly/disassembly. This means the same nominal torque value can produce different actual preload forces under different conditions.
Since D appears as a direct multiplier in the formula, at the same preload force and torque coefficient, doubling the diameter doubles the required torque. In practice, however, larger-diameter bolts are usually designed for higher preload forces too, so the real-world torque difference is usually even larger than the diameter ratio alone.
Knowing the correct tightening torque is the foundation of a joint that’s both safe and long-lasting. Use the calculator above to quickly get a reference value for your own joint, then always cross-check with the manufacturer’s torque table for critical applications.
Related Posts
 What Is Riveting. How Is It Done?
 Friction Materials Used in Clutches
 Dowel Pin Drawings – AutoCAD DWG and PDF
 Pulley Drawings. Pulleys in Technical Drawing
 Five Ways to Cool Roller Bearings
 Bevel Gear Strength Calculations
 Helical Gear Geometry and Strength Calculation
 Gear Calculation Formulas Table